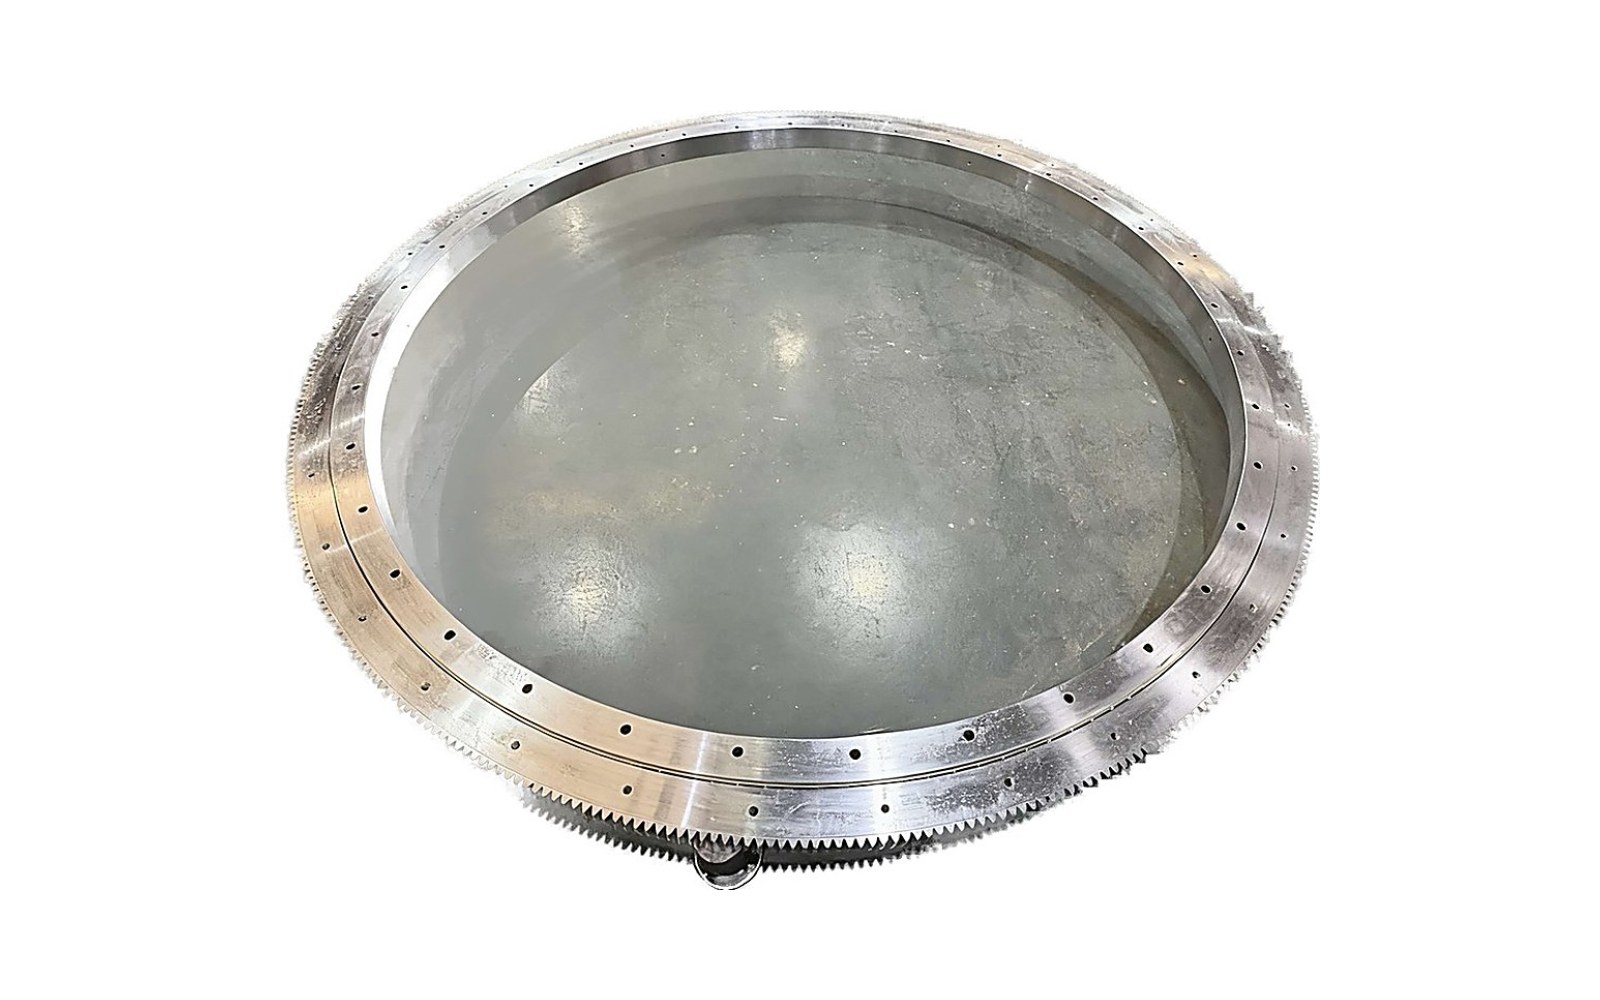
Every ring is inspected before packing. The point is not to produce a certificate — it is to catch a problem while the part is still on our floor and not in a container.
1. Raceway hardness and hardened depth
Readings are taken at several points around the raceway after heat treatment, plus a hardened-depth measurement on a witness piece from the same batch. The soft zone — where the raceway is left unhardened so the gear teeth can be cut — is marked on the ring.
2. Dimensional report
Bore, outside diameter, overall height, raceway diameter and gear parameters are measured against the drawing. Gear runout gets its own check because it shows up as noise in service long before it shows up as wear.
3. Rotation and clearance
The assembled bearing is rotated by hand and then under load for a short run. Starting torque is recorded, and for drives the backlash is measured at several positions.
4. Packing
Rings ship upright on a wooden pallet with the raceway protected, bolts and grease nipples bagged separately, and the documents in a sealed pouch on the outside of the crate.
Want to see what the paperwork looks like?
Request a sample report